
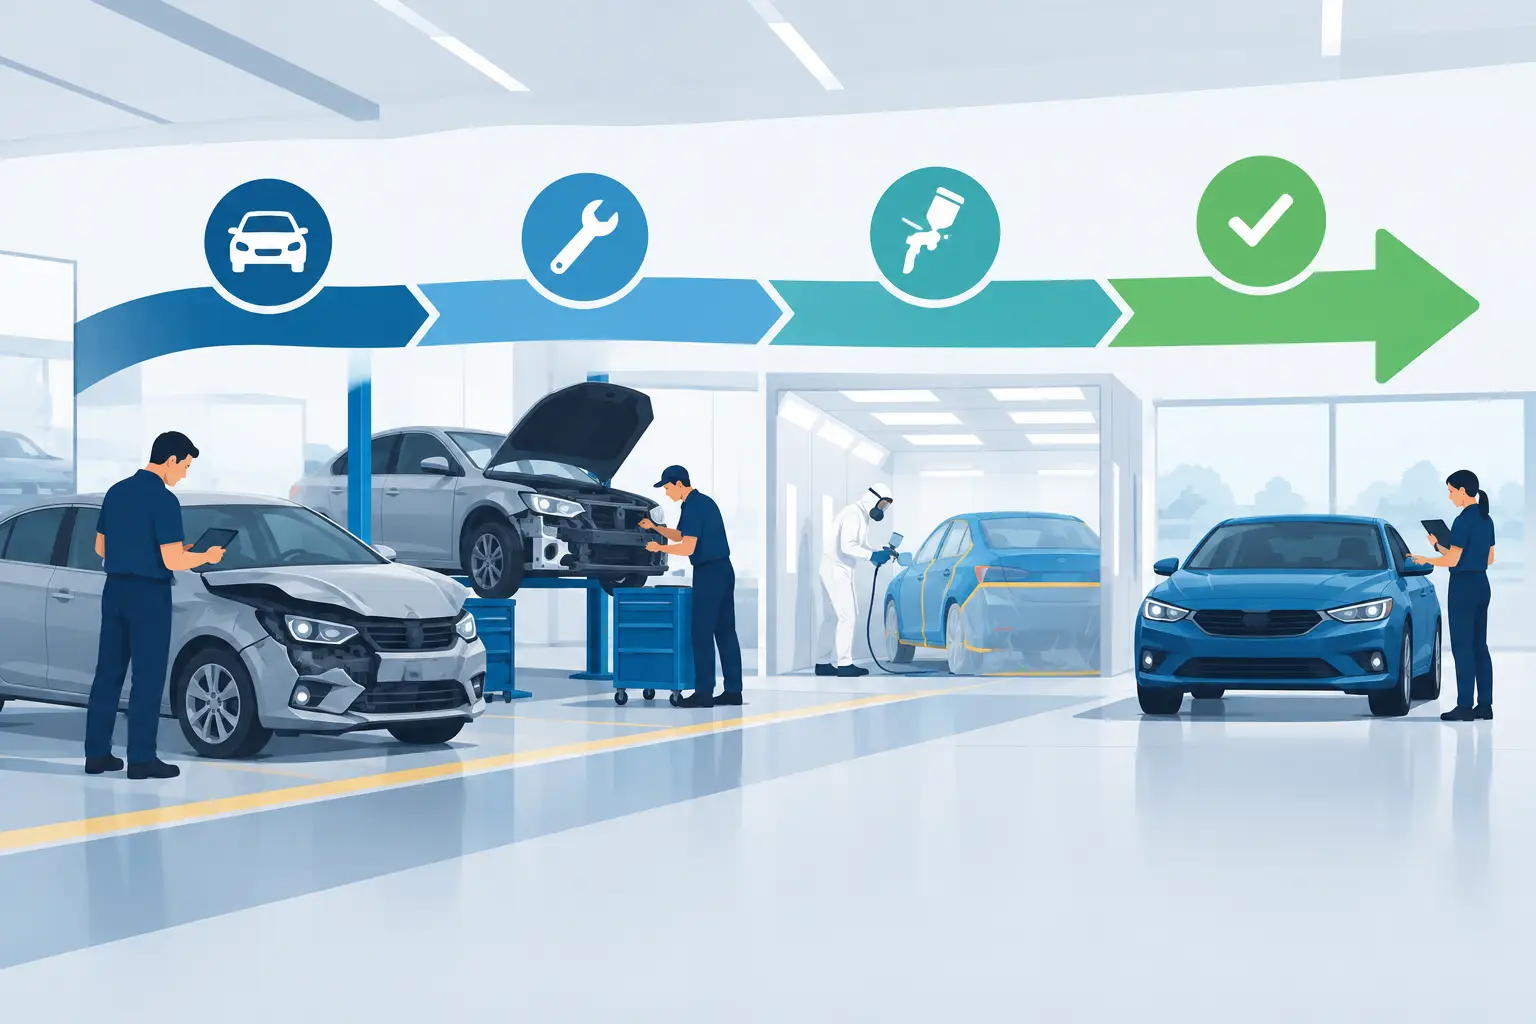
A collision center can look busy while losing money every day. The parking lot is full, technicians are working late, estimators are answering insurer inquiries, and customers are calling for status updates. Yet cycle time expands, supplement volume climbs, rental exposure rises, and gross profit fails to follow sales. A successful collision center turnaround begins by separating visible activity from productive throughput.
For independent operators and multi-shop organizations, the temptation is to treat a weak-performing location as a labor-cost problem. Staffing levels matter, but broad cuts often make a stressed operation worse. Turnarounds work when leadership identifies the constraint that is holding repairs in the building, establishes operating discipline around that constraint, and restores confidence among employees, customers, insurers, and referral partners.
Collision Center Turnaround Begins With the Fact Pattern
Before changing schedules, compensation plans, or vendor relationships, management needs a reliable picture of what is happening on the floor. Many troubled centers operate from lagging financial statements and anecdotal observations. Those are useful signals, but they are not enough to manage a recovery.
Start with the repair order population currently in process. Segment jobs by repair stage, insurer, severity, parts status, age in process, and promised delivery date. A 45-day cycle-time average may conceal two very different problems: a group of straightforward repairable jobs moving reasonably well and a smaller set of parts-delayed or blueprint-incomplete files that are consuming disproportionate space and management attention.
The core measures should connect production to cash and customer impact. Leadership should review touch time, keys-to-keys cycle time, work in process, repair-plan accuracy, supplement frequency, parts availability at blueprint, body and paint labor hours produced, gross profit by department, and delivery-date performance. The objective is not to build a larger dashboard. It is to identify where work stops and why.
Find the Constraint, Not the Loudest Complaint
The loudest complaint in a collision operation is not always the primary constraint. Technicians may point to delayed parts. Parts personnel may point to late supplements. Estimators may point to insurer approval times. Each can be true, but a turnaround requires tracing the sequence back to the first preventable breakdown.
If a vehicle enters production without a complete disassembly, repair plan, scan strategy, and parts order, the parts department will spend the rest of the job reacting. If parts arrive but vehicles have no assigned production date or repair ownership, parts carts become inventory storage. If body repairs are complete but paint has inconsistent staging and prioritization, the paint department becomes the bottleneck.
The answer depends on the shop’s mix. A facility handling high-severity DRP work may need tighter insurer documentation and supplement governance. A shop repairing late-model luxury vehicles may be constrained by OEM parts lead times, calibration access, or specialized technician capacity. A generalized playbook is less useful than an accurate diagnosis.
Stabilize Flow Before Chasing More Volume
A distressed center rarely needs more assignments before it needs better flow. Adding volume to an operation with excess work in process can deepen delays, absorb more administrative labor, and create more opportunities for missed damage and customer dissatisfaction.
The first operational reset is a controlled intake process. Jobs should be scheduled according to available capacity, parts readiness, repair complexity, and the real capacity of downstream departments. That may mean telling a referral source that the center can accept fewer units for a period. It can be an uncomfortable decision, particularly for a shop protecting insurer relationships, but accepting work that cannot be advanced is not capacity growth.
Complete repair planning is the second reset. The blueprint process should establish damage, required operations, structural and mechanical needs, scan requirements, calibration planning, refinish procedures, and likely parts requirements before the vehicle is released into production. Not every supplement is avoidable, especially when concealed damage exists. The standard is not zero supplements. The standard is preventing avoidable interruptions caused by incomplete disassembly, missing documentation, or unresearched repair procedures.
Parts performance deserves the same production rigor as body and paint output. Parts staff need visibility into every ordered component, expected arrival date, return issue, backorder risk, and alternative sourcing decision. A daily parts review should focus on vehicles that can advance today, not merely on a list of open orders. When a critical part is delayed, the production plan must change immediately rather than allowing the vehicle to occupy a stall while waiting.
Rebuild Daily Production Accountability
Daily production meetings are effective only when they produce decisions. A 10-minute stand-up involving production leadership, estimators, parts, paint, and front office staff should review the day’s deliverables, blocked jobs, parts arrivals, supplement approvals, quality-control requirements, and promised dates at risk.
Every stalled job needs one owner and one next action. Vague notes such as waiting on insurance or technician to review do not manage a repair. The team should identify who will contact the carrier, complete the documentation, perform the operation, or revise the delivery promise, along with when that step will occur.
This discipline also protects technicians. In poorly controlled centers, technicians are frequently pulled between jobs because management is trying to keep every vehicle moving. The result is lower touch time, more rework, and frustration among high performers. A defined production plan gives technicians clearer priorities and helps supervisors see when an interruption is caused by planning rather than individual effort.
Protect Margin Through Repair-Plan and Labor Discipline
A turnaround cannot be judged solely on cycle time. Moving vehicles out quickly by discounting repair plans, overlooking required operations, or pushing work through without quality controls simply exchanges an operations problem for a margin and liability problem.
Estimating governance is central. The center should audit closed repair orders for missed labor, refinish operations, scan and calibration charges, sublet recovery, clips and materials, and documented OEM-required procedures. The purpose is not to create conflict with insurers. It is to support complete, safe repairs with consistent documentation and commercial discipline.
Labor productivity requires a similarly direct review. Management should compare hours sold, hours produced, available technician hours, and payroll cost by department. When body labor production is weak, the cause may be technician availability, but it may also be insufficiently planned work, excessive parts interruptions, equipment downtime, or poor job allocation. Wage reductions do not correct those conditions.
Quality must remain visible throughout the recovery. A final quality-control process that catches fit-and-finish defects, warning lights, missed calibrations, or incomplete documentation before delivery will initially expose issues that had been hidden. That is useful. Customer callbacks, rework, and insurer concerns are more expensive than a disciplined pre-delivery review.
Align Claims Communication With the Production Plan
Claims relationships can deteriorate quickly when a shop misses dates without providing credible explanations. Insurers and fleet partners do not expect every repair to proceed exactly as estimated. They do expect timely information, documented supplements, and delivery commitments based on actual repair status.
Estimators should communicate material changes early, particularly for parts backorders, added structural damage, calibration dependencies, or delays requiring rental extensions. The message should describe the issue, the documentation available, the decision needed, and the updated production impact. That is more effective than sending repetitive status notes after a date has already been missed.
Customers need the same clarity in less technical language. A turnaround period can create difficult conversations, but silence is worse. Proactive updates reduce inbound calls, support customer-service scores, and give front-office staff a more credible position when an unavoidable delay occurs.
Use Capital Carefully During the Recovery
Technology, equipment, and outsourcing can improve capacity, but they are not automatic turnaround tools. A new management platform will not fix a center that lacks repair-plan standards. An in-house calibration investment may be justified where volume, vehicle mix, and local vendor performance support it, but it can also create fixed cost and compliance responsibilities that a smaller location is not ready to absorb.
The same applies to hiring. Adding an estimator, parts manager, technician, or production manager may be necessary, but the role should address a measured gap. A center with inconsistent scheduling may need stronger production control before it needs another estimator. A center constrained by paint throughput may need booth utilization changes, prep capacity, or refinish staffing rather than more body technicians.
The First 90 Days Set the Operating Standard
The first phase of a collision center turnaround should focus on containment: stop accepting work beyond realistic capacity, identify aged and blocked repair orders, create daily production accountability, and establish a dependable customer-update process. The second phase should standardize blueprinting, parts control, repair-plan audits, and quality gates. Only after the center has a stable flow should leadership pursue additional volume, major capital investments, or broader market expansion.
For multi-shop operators, a recovery also creates an opportunity to distinguish location-specific issues from systemwide weaknesses. If several centers struggle with supplements, parts visibility, or technician utilization, the answer may be a shared process standard, centralized support function, or revised performance reporting rather than a site-level personnel change.
The strongest turnaround signal is not a single good month. It is a center that can explain where every vehicle stands, what must happen next, who owns that action, and when the customer can reasonably expect delivery. That level of operating control is where restored margin becomes sustainable.