
A misplaced tube of adhesive can turn a profitable repair into a corrosion comeback, a failed calibration event, or an avoidable liability discussion. This guide to automotive adhesive selection is built for the operational reality facing collision centers and mechanical repair businesses: more mixed materials, tighter cycle-time targets, increasingly specific OEM procedures, and less tolerance from insurers or customers for a repair that cannot be documented.
Adhesives are no longer a specialty item reserved for glass work or trim retention. They are part of the repair strategy for bonded panels, structural reinforcements, seam sealing, composite repairs, NVH control, and component retention. Selecting correctly requires more than matching a product name to a familiar job. It requires matching the adhesive system to the vehicle, substrate, joint design, process window, and repair documentation.
Why adhesive selection has become an operating issue
The vehicle mix has changed faster than many repair-process habits. Aluminum, advanced high-strength steel, magnesium, carbon fiber, thermoplastics, and multi-material assemblies all create different bonding and corrosion-control requirements. An adhesive that performs acceptably on a legacy steel panel may be unsuitable for an aluminum-intensive EV structure or a composite liftgate.
For multi-shop operators, variation is a financial concern as much as a technical one. If technicians use different products for similar repairs, stores can experience inconsistent cure times, rework, inventory waste, and uneven quality-control outcomes. That variability also complicates estimating, training, and insurer conversations when a procedure requires a specific adhesive category or preparation sequence.
The first principle is straightforward: OEM repair information controls the decision. Product manufacturers provide valuable technical data, but a product data sheet does not override an automaker’s repair procedure. When the OEM specifies an adhesive type, a bonding method, a primer, a corrosion-protection step, or a replacement-only component, the repair plan needs to reflect that instruction.
Start with the repair objective, not the cartridge
A disciplined selection process begins by defining what the adhesive must accomplish. Structural bonding, panel bonding, seam sealing, glass installation, plastic repair, and NVH treatment can all involve two-component products, but they are not interchangeable applications.
Structural bonding and crash performance
Structural adhesives contribute to stiffness, energy management, fatigue resistance, and load transfer in designated areas. Their use often intersects with weld bonding, rivet bonding, or other mechanical fastening specified by the OEM. A structural adhesive should never be selected based solely on strength numbers printed on a package. Joint geometry, bond-line thickness, cure profile, substrate preparation, and the required combination of fastening methods determine performance.
This category deserves heightened controls. Verify whether the manufacturer permits sectioning, whether heat affects nearby materials or corrosion protection, and whether the repair requires a particular adhesive with a defined working time. On late-model vehicles, repair documentation should identify the procedure source, adhesive product, lot information where required, and cure conditions.
Outer-panel and non-structural bonding
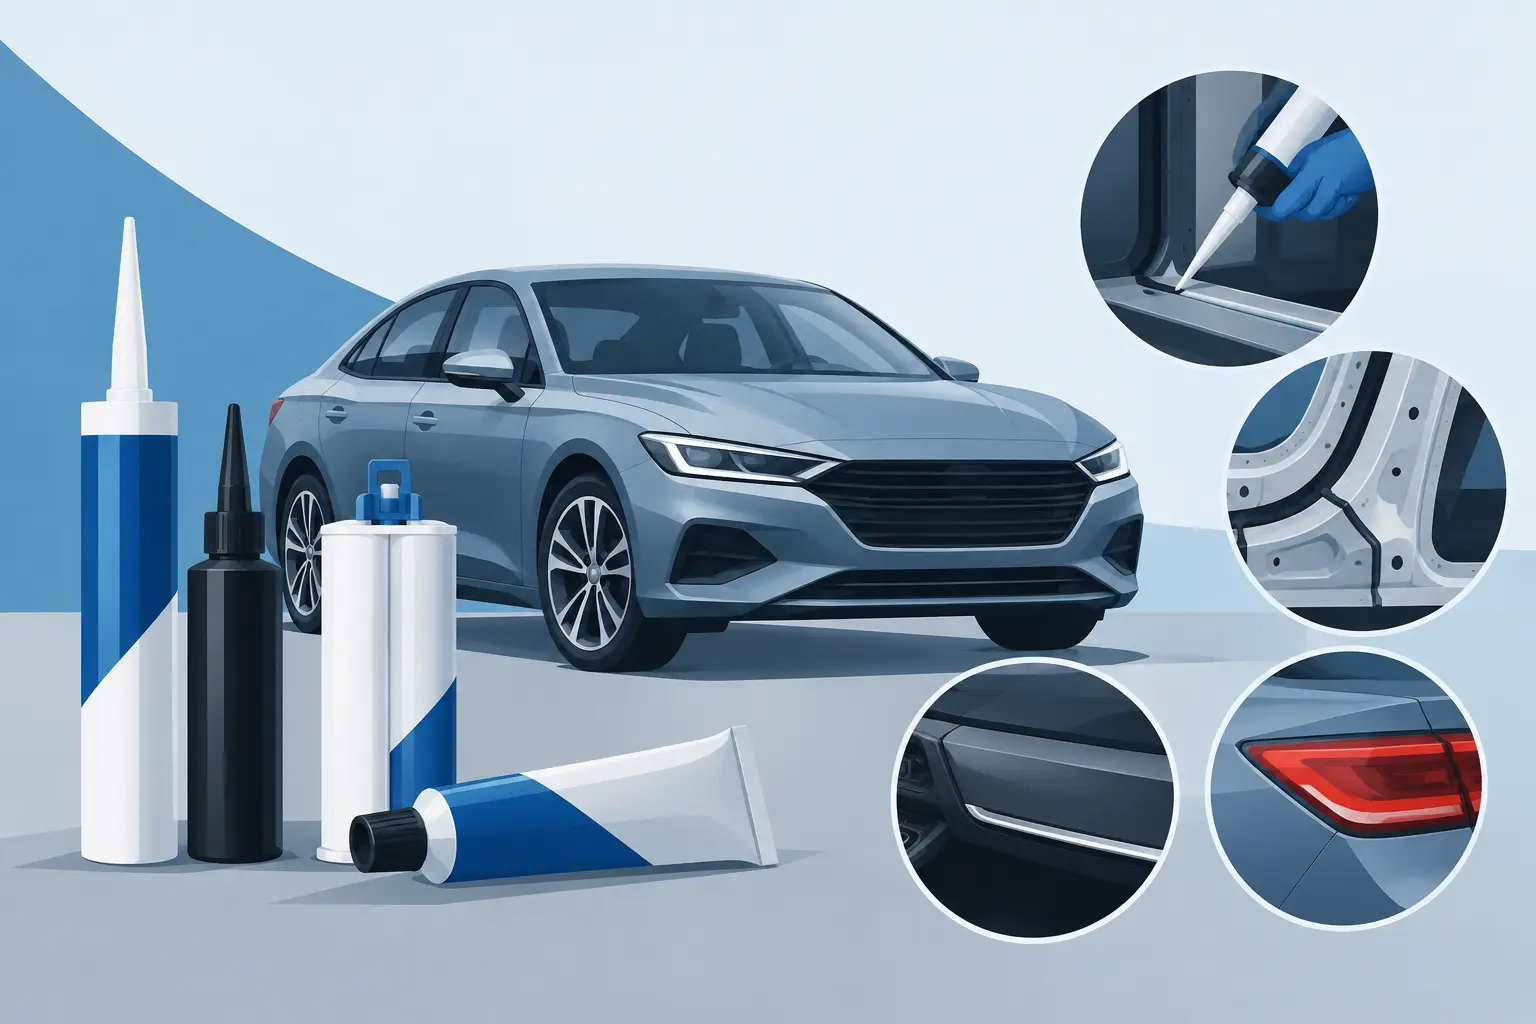
Panel bonding adhesives are commonly used for non-structural exterior panels where OEM procedures permit adhesive replacement instead of welding. The commercial benefit can be substantial: reduced heat distortion, lower risk of damaging adjacent coatings, and less time spent correcting weld-related issues.
The trade-off is that panel bonding remains process-sensitive. Flange fit, adhesive bead size, clamping pressure, open time, and corrosion protection are not optional details. Excessive squeeze-out can signal an inadequate bond line, while insufficient squeeze-out may indicate incomplete contact. Technicians also need to understand where adhesive cannot substitute for specified welds, rivets, or other attachments.
Glass, sealing, and water management
Automotive glass urethane is a safety-related adhesive system, not a generic sealant. Safe drive-away time depends on the product, temperature, humidity, glass configuration, and the vehicle’s restraint-system requirements. A windshield installation that overlooks primer compatibility, contamination control, or cure conditions can create water leaks, wind noise, corrosion, and occupant-protection exposure.
Seam sealers serve a different purpose. They manage water, dust, and air intrusion while restoring the appearance and flexibility of factory seams. Shops should distinguish between brushable, sprayable, self-leveling, and heavy-bodied products based on the original seam design and paint process. Using a hard product where the OEM seam needs movement can lead to cracking after delivery.
The guide to automotive adhesive selection: five checks
A useful shop-level framework is to run every adhesive decision through five checks before work begins.
First, confirm the OEM procedure and repairability statement. Identify whether bonding is allowed, where it is allowed, what companion fasteners are required, and whether the procedure specifies a material or brand family.
Second, identify every substrate in the joint. Steel, galvanized steel, aluminum, composite, SMC, plastic, e-coat, bare metal, and previously repaired surfaces may each demand different preparation. Mixed-metal joints also raise galvanic-corrosion concerns. Adhesive can help isolate materials, but only when the specified coatings and bond-line controls are maintained.
Third, assess the joint and its service environment. Consider peel, shear, vibration, thermal cycling, moisture exposure, chemical exposure, and movement. A rigid epoxy may be well suited to one joint but inappropriate where flexibility is needed. A plastic-repair adhesive must also match the substrate identification and expected flex characteristics.
Fourth, validate the process window. Working time, fixture time, cure time, temperature requirements, cartridge conditioning, mixing ratio, and applicator setup directly affect throughput. A fast-cure product may shorten a stall’s occupancy time, but it can be a poor fit if the technician cannot position a large panel before the product begins to set.
Fifth, confirm documentation and quality-control requirements. The repair file should show the procedure followed and, where applicable, the product used, cure conditions, and technician signoff. This supports internal accountability, customer communication, insurer file integrity, and future liability defense.
Substrate preparation is where margins are won or lost
Many adhesive failures are preparation failures. Oils, mold-release agents, sanding residue, fingerprints, oxidation, old adhesive residue, and incompatible cleaners can compromise an otherwise correct product choice. The exact preparation sequence must come from the OEM procedure and adhesive technical documentation, particularly on aluminum and composite surfaces.
A common operational mistake is treating sanding grit, cleaner, primer, and application method as interchangeable between product lines. They are not. One system may require bare-metal preparation and a corrosion-control coating; another may require bonding over a specified e-coat condition. Some plastics require flame treatment or an adhesion promoter, while others should not be aggressively sanded.
Equipment condition matters as well. Expired cartridges, improperly stored materials, damaged mixing nozzles, and mismatched applicators introduce preventable risk. Standardizing dispensing tools and storage practices across locations makes quality more repeatable and reduces the temptation to improvise when a job reaches the repair floor.
Build adhesive controls into estimating and production
Adhesive selection should begin at blueprinting, not when the vehicle is already in a stall. Estimators need enough process knowledge to flag bonded panels, glass operations, aluminum repairs, plastic components, and OEM-required materials. That does not make the estimator responsible for replacing technician judgment. It ensures the estimate, parts plan, repair plan, and production schedule account for the work.
Labor operations should reflect substrate preparation, removal of existing adhesive where required, corrosion protection, adhesive application, clamping or fixturing, cure time, and any related calibration or validation steps. Missing these items creates a familiar downstream problem: the job looks complete on paper but cannot move without an unpaid delay or a process shortcut.
For insurers and repairers, clarity helps. Documentation should explain why a named adhesive or procedure was necessary rather than presenting a material line with no connection to the repair plan. The strongest files tie the operation to vehicle-specific instructions and demonstrate that the repairer managed the required process.
Inventory strategy should favor control over variety
A broad adhesive cabinet can look like preparedness, but it often produces expired inventory, technician confusion, and uncontrolled substitution. Shops generally benefit from a standardized core assortment tied to their vehicle mix, OEM certifications, refinish system, and repair capabilities.
That does not mean every location should carry the same products without exception. A facility performing high volumes of glass work, aluminum repair, commercial vehicles, or plastic reconstruction may require specialized materials. The goal is a controlled exception process, not an unlimited assortment.
Review consumption, expiration dates, emergency purchases, rework events, and vendor support at regular intervals. These measures reveal whether the shop has a product problem, a training problem, or a planning problem. They also give procurement leaders better leverage when discussing stocking arrangements, technical support, and supply continuity with distributors.
Training must connect chemistry to production behavior
Technicians do not need a chemistry lecture to make sound decisions, but they do need to understand why open time, cure temperature, mix ratio, bead profile, and surface condition matter. Training that only demonstrates how to dispense a cartridge will not prevent shortcuts under production pressure.
The most effective programs combine product instruction with real repair scenarios: a bonded quarter panel, an aluminum-to-steel interface, a windshield replacement with ADAS considerations, and a thermoplastic bumper repair. Supervisors should reinforce the same controls through repair-plan reviews and quality checks, especially after new product introductions or OEM procedure changes.
Adhesive selection is ultimately a capacity and risk-management decision. The right material, applied through the right procedure, protects repair quality while keeping the schedule credible. When a shop treats adhesive controls as part of its operating system rather than a consumables decision, it is better positioned to defend the repair, reduce rework, and keep increasingly complex vehicles moving through the business.