
A refinish department can look busy, hit its sales target, and still lose margin through material consumption that is never measured against the work produced. Knowing how to calculate paint usage turns a monthly material invoice into an operating metric: one that can expose estimating gaps, process variation, poor mix discipline, and changes in vehicle repair complexity.
For collision operators, the objective is not to force every repair into a single paint-cost number. A bumper cover, a three-stage pearl blend, and a minor conventional-panel repair carry different material requirements. The practical goal is to establish an expected range for each repair type, then identify exceptions quickly enough to correct them.
Start With the Right Definition of Paint Usage
Paint usage is often discussed as gallons or dollars purchased in a month. That is useful for cash-flow planning, but it is not a complete production measure. Purchased material may include inventory build, price changes, returns, toners, hardeners, reducers, clearcoat, abrasives, masking products, and other consumables that do not all move through the booth at the same rate.
For production control, distinguish between three measures. Mixed material is the amount prepared at the scale. Sprayed material is the amount that leaves the gun. Applied material is the portion that actually reaches and remains on the repair surface at the specified film build. The gap between those numbers is where transfer efficiency, overspray, cup residue, test panels, rework, and disposal costs reside.
A shop should track both volume and dollars. Volume helps identify process changes even when supplier pricing moves. Dollars show the margin impact. For multi-shop operators, using both measures also avoids misleading comparisons between locations that use different paint lines, labor rates, or repair mixes.
How to Calculate Paint Usage by Repair Area
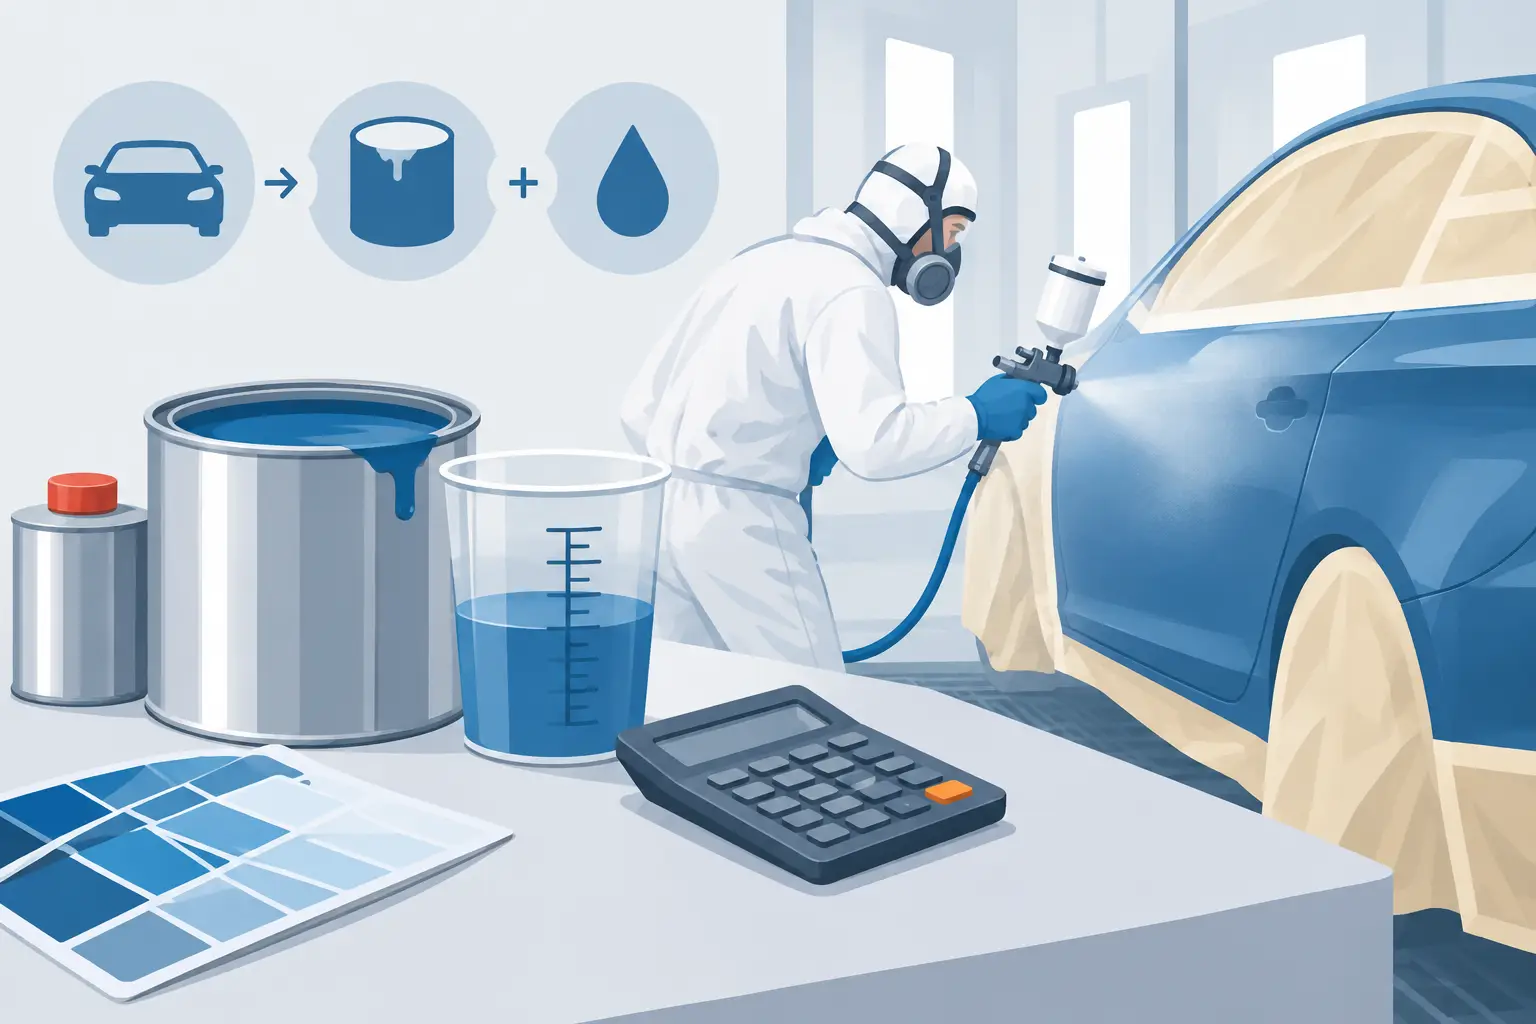
The basic calculation begins with panel area and a product’s stated sprayable coverage. In simplified form:
Required ready-to-spray material = repair area ÷ coverage rate ÷ transfer efficiency adjustment
Coverage data should come from the product technical data sheet, not from a generic rule of thumb. A coating may be rated for a stated square-foot yield at a defined dry-film thickness, reduction ratio, and number of coats. The figure can change materially when the technician needs additional hiding coats, uses a sealer, or sprays a color that requires a different groundcoat.
Consider a repair requiring color and clear over 80 square feet of prepared and blended surface. If the selected basecoat has a theoretical sprayable coverage of 600 square feet per gallon, the starting basecoat requirement is 0.133 gallon, or roughly 17 fluid ounces, before accounting for losses. At an assumed 65% transfer efficiency, the adjusted volume is about 26 fluid ounces of ready-to-spray material.
That calculation is a planning baseline, not a booth instruction. The actual mix must account for the paint system’s mix ratio. A 1:1 basecoat mix, for example, means the ready-to-spray amount includes both color and reducer. Clearcoat may use a different ratio, a different coverage rate, and a different film-build target. Estimators and production managers should avoid treating a ready-to-spray ounce as equivalent to an ounce of unreduced color.
Measure the refinished surface, not just the damaged panel
The largest estimating error is often the failure to account for the true spray area. A repair may be confined to one door, but color may need to extend into adjacent panels for blendability. A bumper repair can require nearly full-cover refinishing because of material type, damage location, texture, or color match limitations. Edges, jamb returns, mirror caps, moldings, and R&I decisions can all expand the masked and sprayed area.
Panel databases, estimating-system refinish times, and shop-specific panel-area tables provide a workable starting point. The most reliable operations validate those references against their own paint-mixing records. Over time, the data will show where theoretical panel dimensions diverge from actual repair practice, particularly on late-model SUVs, pickups, EVs, and vehicles with complex bumper and trim configurations.
Build a Formula That Reflects Shop Conditions
A usable internal model needs more than square footage. It should include the variables that materially change usage: number of refinish panels, blend panels, coating system, color family, repair method, and expected number of spray cycles.
A practical job-level formula is:
Expected material cost = substrate products + color + clearcoat + additives + allocated waste and consumables
Each category should be calculated from expected ready-to-spray volume and the current mixed cost per ounce. That mixed cost matters because it captures toners, activators, reducers, flex additives, and other ingredients required to produce sprayable material.
Waste should be an explicit factor rather than an unexplained variance at month-end. A facility using reusable cups and disciplined mix planning may operate with lower residual loss than a facility using disposable liners and routinely mixing to cover uncertainty. Neither condition is automatically right or wrong. The point is to measure it, set a reasonable target by job type, and understand the operational reason when it moves.
For example, a 10% to 15% allowance may be reasonable for controlled, repeatable work, while low-volume custom colors, three-stage finishes, and difficult color-match repairs can require a larger reserve. Applying one universal waste percentage to every repair can hide both avoidable overmixing and legitimate complexity.
Transfer efficiency is a management assumption, not a fixed fact
Transfer efficiency is influenced by gun setup, atomization, booth airflow, technician technique, spray distance, part orientation, and the geometry of the repair. A flat hood and a heavily contoured bumper do not behave the same way. Nor do horizontal and vertical surfaces.
HVLP and compliant spray equipment can improve transfer performance, but equipment alone does not establish actual efficiency. Training, preventive maintenance, air quality, and consistent setup matter. If a location’s calculated consumption rises without a shift in repair mix, managers should check gun performance, booth conditions, and technician practices before assuming the paint line has become more expensive.
Reconcile Calculated Usage With Inventory and Estimates
The operational value emerges when calculated usage is reconciled every week or month. Start with beginning inventory, add purchases, subtract ending inventory, and adjust for returns, transfers, and known non-production usage. That produces actual material consumption for the period.
Then compare actual consumption with the sum of expected job-level material usage from completed repair orders. The variance should be reviewed alongside paint sales, refinish hours, repair order count, supplement frequency, and the percentage of blend operations. A single ratio, such as paint-material cost as a percentage of refinish sales, is useful but insufficient on its own. A higher percentage may reflect poor control, but it may also reflect a period with more complex color work, a higher bumper mix, or delayed insurer material-rate updates.
Estimating accuracy deserves separate attention. If the shop’s mix records consistently exceed estimated material allowances on certain repair categories, the answer may be a better estimating rule, a revised blend policy, or stronger documentation for billable operations. If the mix record exceeds the allowance only for certain technicians or shifts, the issue is more likely process discipline or training.
Use the Data to Protect Throughput and Margin
Paint usage data should not become a technician scorecard detached from quality. A technician who mixes too little may create delays, contamination risk, or color-match problems. A technician who mixes more than the theoretical minimum may be managing a legitimate difficult color. Review exceptions with the repair file, mix label, and vehicle context before assigning a cause.
The most productive reporting separates normal complexity from controllable loss. Track material dollars per refinish hour, ready-to-spray ounces per panel, waste volume per job, and actual-versus-expected material cost. Segment results by color complexity, repair type, and location. For MSOs, comparable definitions and disciplined inventory counts are essential before ranking facilities.
This approach also strengthens supplier conversations. When a distributor recommends a new clearcoat, faster reducer, or alternative mixing system, a shop with usable consumption data can evaluate the change on total applied cost, cycle time, rework exposure, and waste – not merely on the price of a gallon.
The next step is straightforward: select a representative group of completed repairs, calculate expected usage from verified panel area and product data, and compare it with the mix-room record. The first variance report will rarely be perfect. It will, however, show where paint consumption is a cost of doing business and where it is a solvable operating issue.